What Is Custom Zinc Alloy Die Casting and How Does It Work?
Custom Zinc Alloy Die Casting is a manufacturing process for producing precise metal components at scale. It uses heated zinc alloy, reusable steel dies, and controlled injection pressure. The method supports complex shapes, thin walls, smooth surfaces, and consistent dimensions.
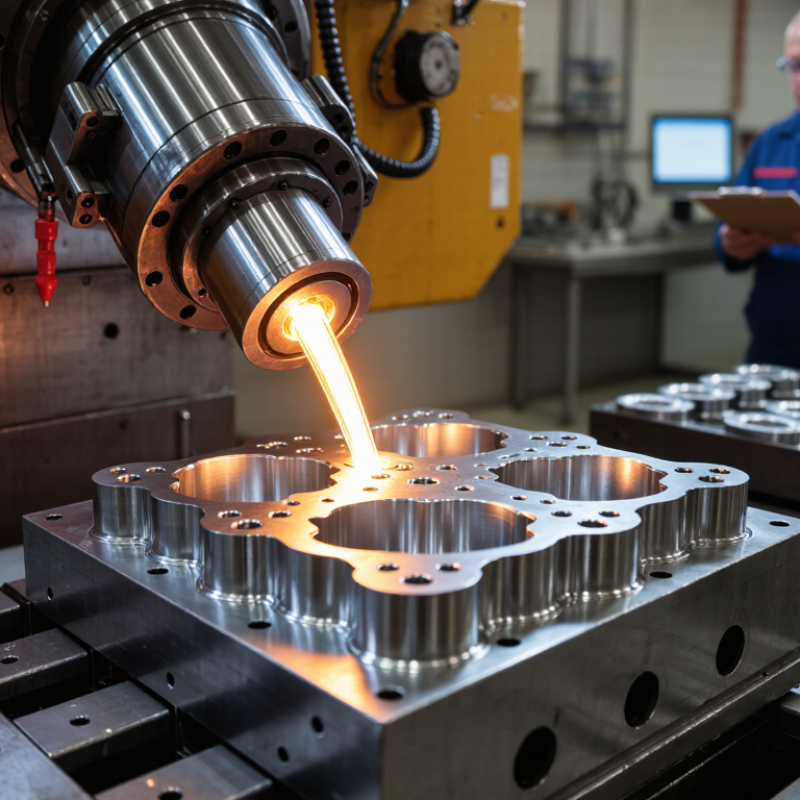
The process begins with a carefully designed die based on the component’s function. Engineers consider wall thickness, draft angles, filling paths, cooling, and ejection points. Molten zinc alloy then enters the closed die at high speed. Pressure holds the metal against the cavity walls. It solidifies quickly. The die opens, and ejector pins release the casting.
That is the basic mechanism.
In practical production, quality depends on more than machine pressure. Alloy selection, die temperature, lubrication, cycle timing, and venting can affect porosity and surface defects. Trimming removes excess material from gates and flash. Further operations may include machining, polishing, plating, powder coating, or dimensional inspection. Reliable manufacturers use drawings, material certificates, process controls, and sampling records to verify performance.
The process is not flawless. Small design changes can create filling problems or premature die wear. A visually attractive part may still contain hidden voids. Engineers should review stress requirements, tolerance limits, corrosion exposure, and expected production volume before approving a design. Better decisions come from prototypes, testing, and honest communication between designers, foundries, and customers. This guide explains how Custom Zinc Alloy Die Casting works, where it performs well, and which practical details deserve closer attention.
What Custom Zinc Alloy Die Casting Means
Custom zinc alloy die casting means producing a metal part around a specific design, not selecting a standard shape. Zinc alloy is heated until it becomes fluid, then injected into a reusable steel mold under controlled pressure. The mold forms details such as ribs, holes, logos, and textured surfaces. After cooling, the casting is trimmed, inspected, and sometimes finished with plating or coating.
The word custom covers more than appearance. It includes the part’s dimensions, wall thickness, strength needs, surface quality, and production quantity. An experienced engineer checks draft angles and flow paths before tooling begins. These details help the metal fill narrow sections and release from the mold cleanly. In practice, small design changes can reduce porosity, flash, and costly rework. A drawing may look perfect on screen. Manufacturing can disagree.
Quality depends on repeatable temperatures, injection pressure, mold maintenance, and dimensional inspection. Measuring critical points with gauges or coordinate equipment provides stronger evidence than visual checks alone. Still, inspection plans should match the part’s real function. Measuring everything may waste time, while checking too little creates risk.
Tips: Share clear 3D files, tolerances, and expected quantities early. Ask about wall thickness, draft angles, and finishing options. Request sample parts before approving large-scale production. Keep a record of inspection results, even when the first batch seems acceptable. Small defects sometimes appear later.
How Alloy Selection and Part Design Shape the Casting
What Is Custom Zinc Alloy Die Casting and How Does It Work?
How Alloy Selection and Part Design Shape the Casting
Custom zinc alloy die casting injects molten metal into a hardened steel mold under high pressure. The alloy choice controls fluidity, strength, surface finish, and cycle stability. Common zinc die-casting alloys contain roughly 3.5% to 4.3% aluminum, according to technical data from the International Zinc Association. Small chemistry changes can affect filling behavior and dimensional results.
Part design matters just as much. Thin walls may reduce weight, but they can freeze before the cavity fills. Sharp internal corners create stress and restrict metal flow. Designers usually add generous radii, balanced wall sections, and short flow paths. Ejection pins also need planned locations. A visually clean model may still trap air or cause uneven shrinkage.
The U.S. Geological Survey reported about 12 million metric tons of global zinc mine production in 2024. That scale supports a mature supply chain, but it does not guarantee consistent casting quality. Melting temperature, die temperature, lubrication, and recycled-content control still require practical monitoring. No alloy is perfect.
Tips: Define strength, corrosion exposure, and surface requirements before choosing the alloy. Use simulation to review filling and cooling, then confirm results with trial shots. Keep gates away from critical cosmetic surfaces. A small design change can prevent a large tooling problem.
How Molten Zinc Becomes a Custom Metal Component
Custom zinc alloy die casting begins with small ingots, not a finished component. The alloy is melted at roughly 380–430°C, depending on its composition. A heated chamber then pushes the molten metal into a hardened steel die under high pressure. It fills narrow ribs, bosses, and textured surfaces within milliseconds. The die opens after solidification, and ejector pins release the casting.
The process is fast, but not forgiving. Poor venting may trap air near a thin wall. Excessive lubricant can mark a polished surface. Engineers adjust injection speed, pressure, die temperature, and cooling time through trial shots. That practical feedback matters more than a perfect computer model. The International Lead and Zinc Study Group reported approximately 13.6 million tonnes of refined zinc usage in 2023, showing the scale behind this widely used material system. The U.S. Geological Survey’s Mineral Commodity Summaries 2024 recorded about 12 million tonnes of global zinc mine production in 2023.
After ejection, operators trim runners and inspect dimensions, pores, flash, and surface finish. X-ray inspection may reveal internal voids that calipers cannot detect. Zinc’s low melting temperature supports short cycles and detailed shapes, while its natural dimensional stability suits housings, handles, and mechanical fittings. Still, every custom die has limits. Very thin sections may cool too early, and sharp internal corners can disturb metal flow. Good design leaves room for the alloy to move.
How Cast Parts Are Finished and Quality-Checked
Custom zinc alloy die casting begins with molten alloy injected into a steel mold under high pressure. The metal fills narrow ribs, holes, and detailed surfaces within seconds. After ejection, operators remove runners, gates, and flash from each cast part. Trimmed edges are deburred by hand or with vibratory equipment.
The finishing method depends on the part’s function and appearance. Tumbling can smooth sharp edges, while shot blasting creates a uniform matte texture. Machining may improve threaded holes or tight mating surfaces. A protective coating can also reduce oxidation and improve handling durability. Appearance is only one concern.
Quality checks Quality checks start with visual inspection under controlled lighting. Inspectors look for cracks, cold shuts, dents, trapped debris, and uneven coating. Calipers, gauges, and coordinate measuring equipment verify critical dimensions. Thread gauges test holes, while sample sections may reveal internal porosity. Production records should connect inspection results with mold settings, alloy temperature, and trimming conditions.
In practical casting work, a bright surface can still hide a dimensional problem. No inspection method is perfect. That deserves honest review. Sampling can miss a defect when process variation is unstable, so critical parts may require more frequent checks. When measurements disagree, experienced technicians should pause production, recheck the equipment, and examine the part again rather than accept convenient data.
Where Custom Zinc Die Castings Are Used and What Limits Them
Custom zinc alloy die casting is chosen when manufacturers need detailed, repeatable metal parts at medium or high volumes. Molten alloy enters a hardened steel die under pressure, filling narrow ribs, lettering, and mounting bosses. After cooling, ejector pins release the part for trimming, inspection, and finishing. This controlled cycle can reduce machining and maintain consistent dimensions across thousands of pieces.
Common applications include lock housings, appliance controls, lighting components, automotive interior hardware, and electronic enclosures. Zinc castings also suit handles, brackets, small gear cases, and decorative fittings requiring smooth surfaces. Their density gives products a solid hand feel, while thin sections can reduce material use. They are practical.
However, custom tooling requires upfront cost and careful engineering. Very large parts may be uneconomical, while extremely thin walls can cause incomplete fills or fragile edges. Designers need draft angles, steady wall thickness, sensible radii, and shrinkage allowances. High operating temperatures can reduce strength and accelerate dimensional change, so zinc is unsuitable near severe heat sources. Corrosive environments may require plating, coating, or sealing.
In practical reviews, attractive prototypes sometimes fail because hidden pockets trap air during filling. That detail is easy to miss. Inspection should check porosity, threads, flatness, and coating adhesion, not only appearance. A polished sample can hide production risks.
What Is Custom Zinc Alloy Die Casting and How Does It Work?
Typical ultimate tensile strength of common zinc die-casting alloy grades
Where custom zinc die castings are used: Zinc die castings are commonly selected for housings, brackets, locks, handles, gears, connectors, small structural parts, and components requiring accurate dimensions, thin walls, good surface finish, and high production efficiency.
What limits them: Zinc alloys are generally less suitable for continuous high-temperature service, highly corrosive environments without suitable protection, and applications requiring very low weight or the highest structural strength. Actual performance depends on alloy grade, part geometry, wall thickness, surface treatment, and casting conditions.
Representative room-temperature values for common zinc die-casting alloy grades; published values can vary according to testing standards and section thickness.